Conveyor Types We Manufacture and Service
We design, manufacture, and install various conveyor types in New York, NY. With years of industry experience, we take pride in delivering tailored, high-performance solutions engineered to boost your productivity and streamline your workflow. Whether you’re in food and beverage or any other industry, you can count on us for unmatched products that feature efficiency, safety, and flexibility that drive your business forward.
Explore the conveyor types we engineer and service to discover the perfect fit for your operation. Elevate your processes today with conveyor solutions built for success.
Modular Design and Space Optimization
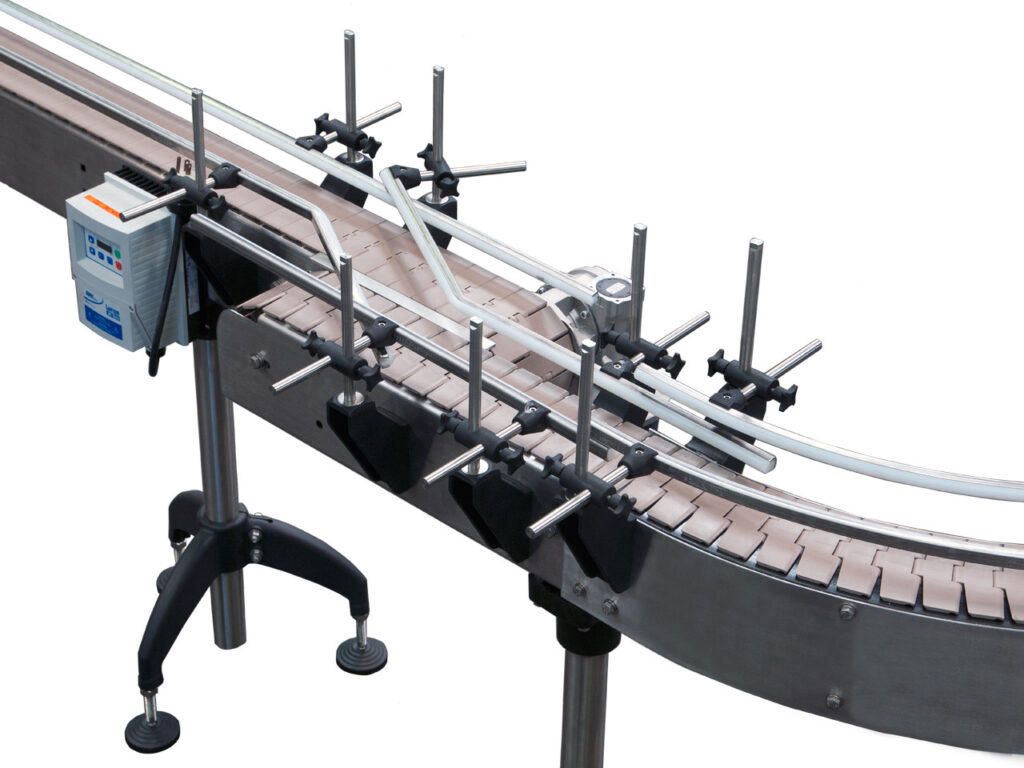
Utilizing modular, pre-fabricated components, our tabletop conveyors enable seamless, safe, and efficient field installations and modifications, minimizing operational downtime. To address specific spatial requirements, we offer low-profile drives and tight-radius curves that can navigate both vertical and horizontal planes. Additionally, our solutions include spiral and multi-level configurations that effectively verticalize your processes. This approach optimizes floor space usage, maintaining clear and safe pathways for personnel, forklifts, pallet jacks, and other mobile equipment within your production facility.
Custom Engineering and Automation Integration
Our team of engineers will conduct a thorough assessment of your operations to provide tailored recommendations that enhance production efficiency. We offer complete conveyor line design services to meet your unique specifications, integrating advanced automation components, including combiners, dividers, turners, loop inverters, and more.
Tabletop Conveyors
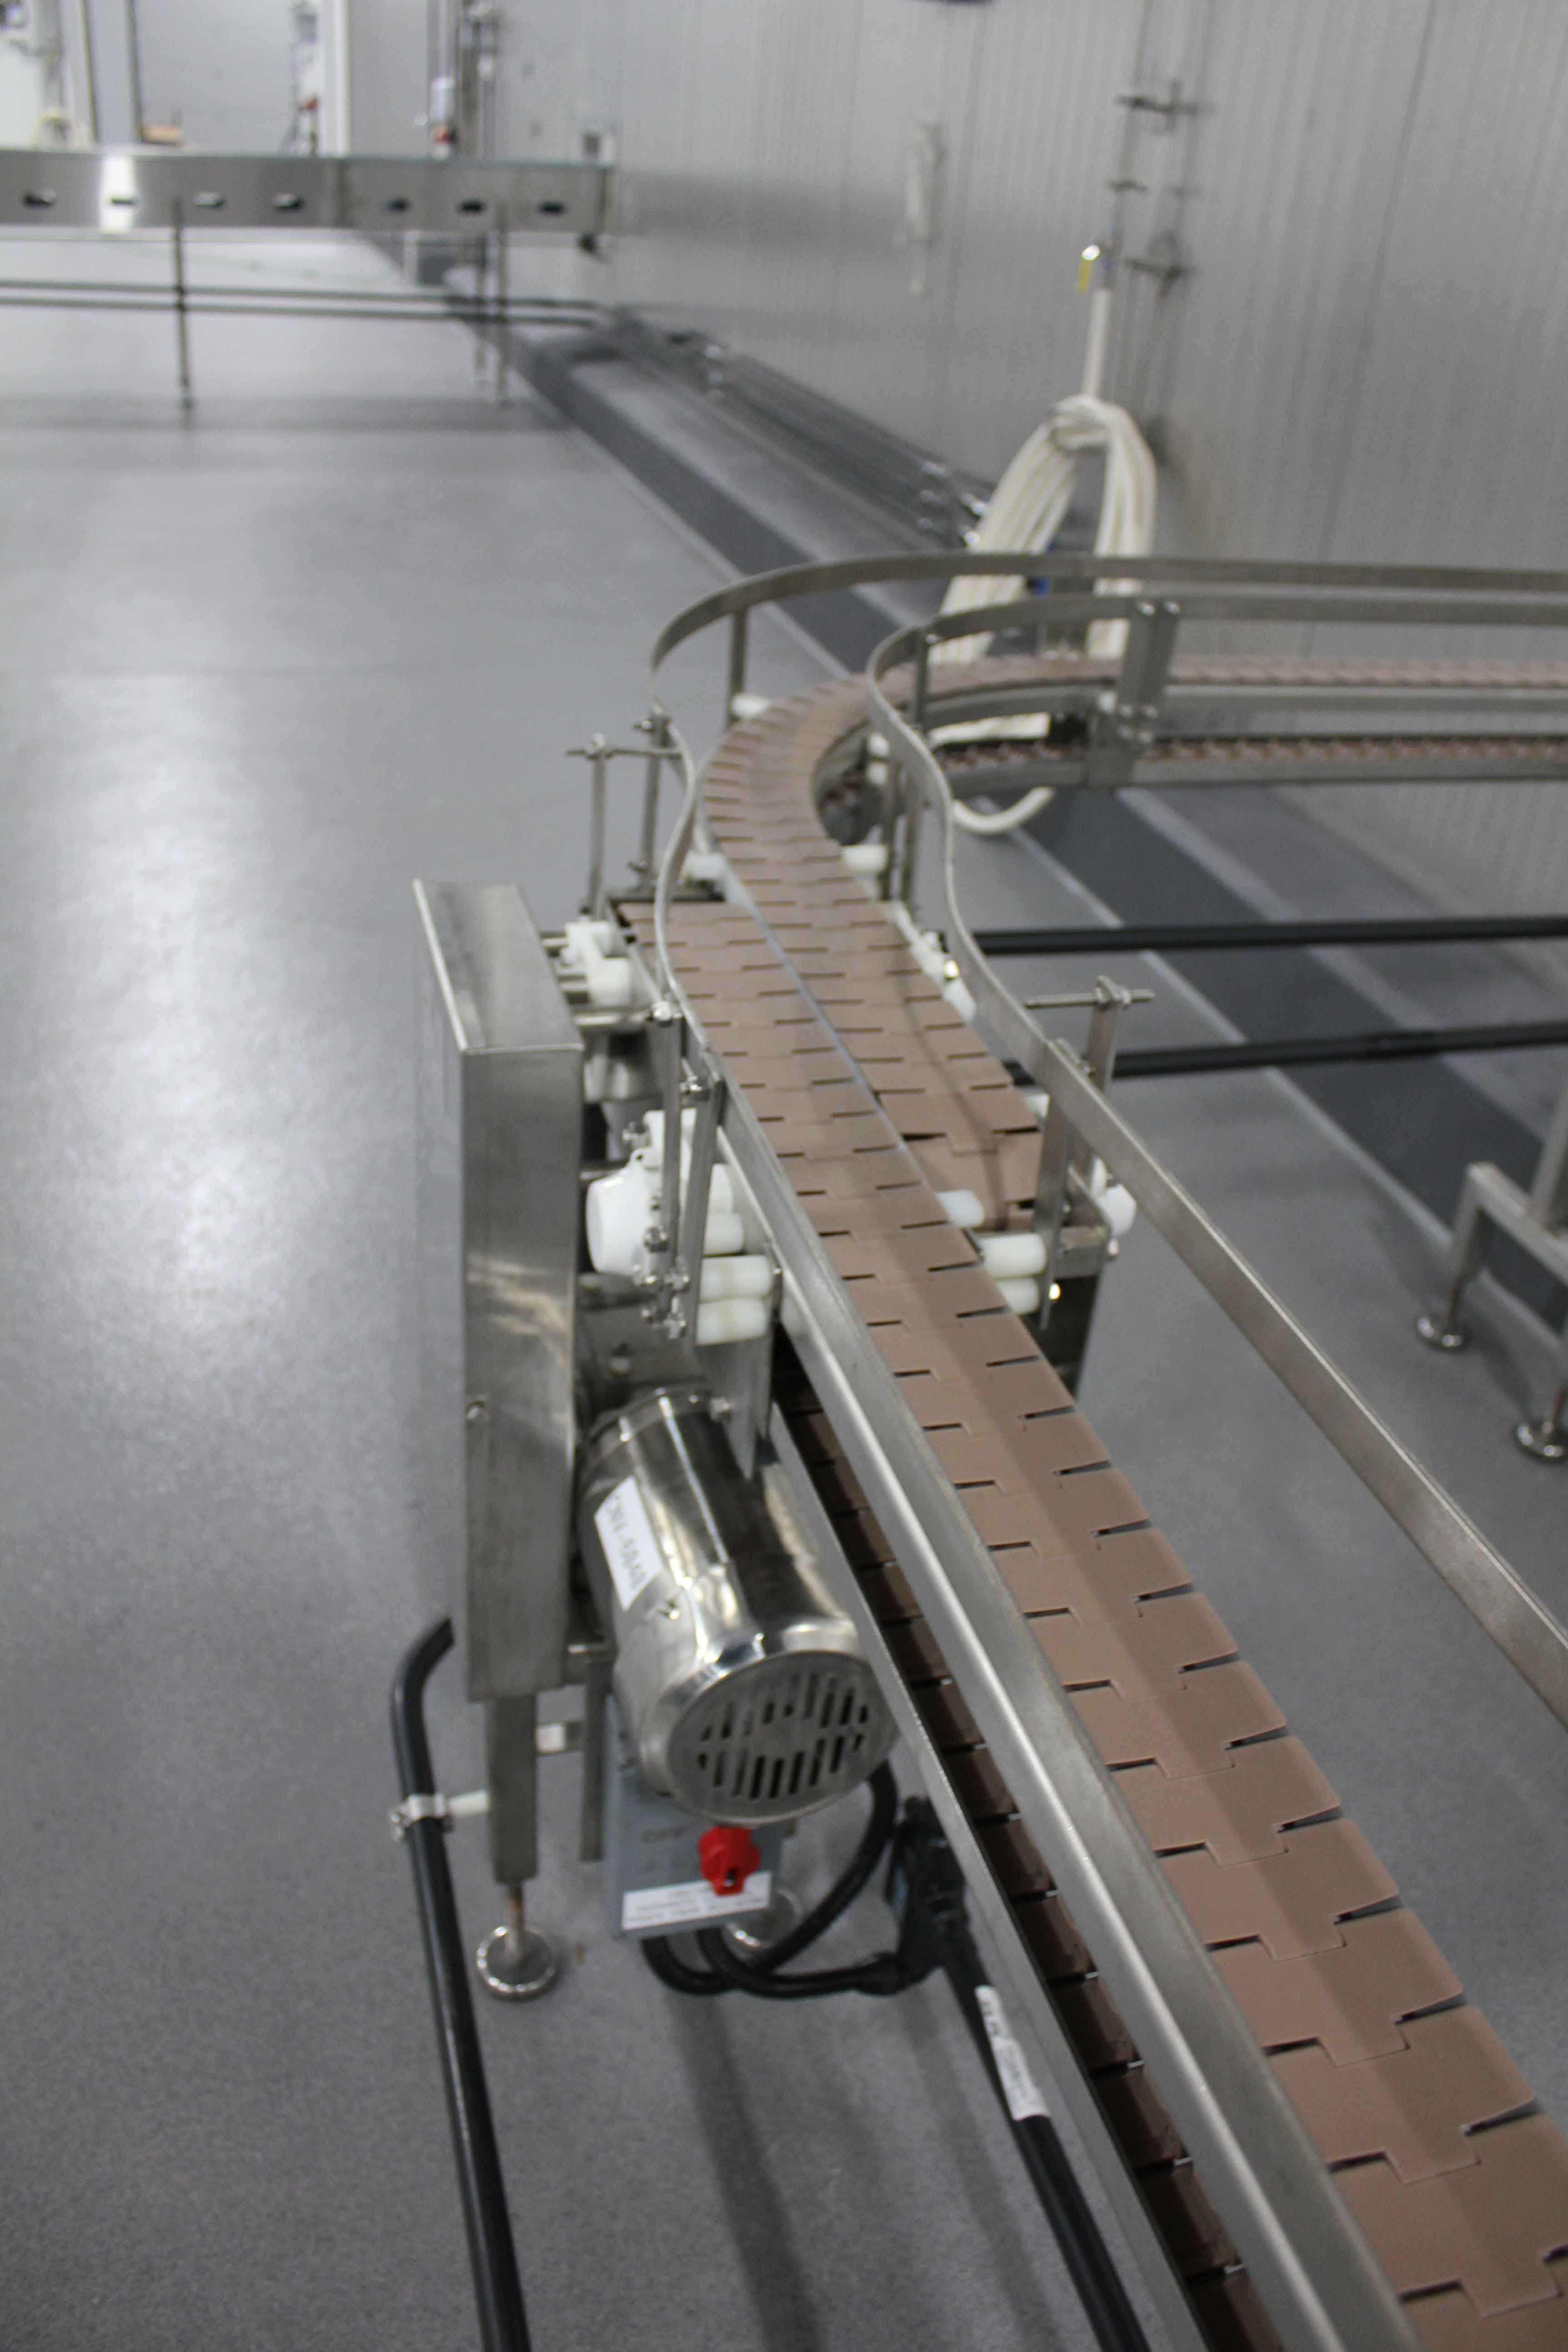
Tabletop conveyors are among the most widely used conveyor systems for transporting individual products, such as empty or filled bottles, jars, small boxes, packages, and other containers. Our tabletop conveyors feature robust stainless-steel frames paired with durable plastic belts, making them ideal for a broad spectrum of industrial applications. All units are constructed to sanitary-grade standards and are well-suited for operation in hot, cold, and high-moisture environments.
Mat Top Conveyors
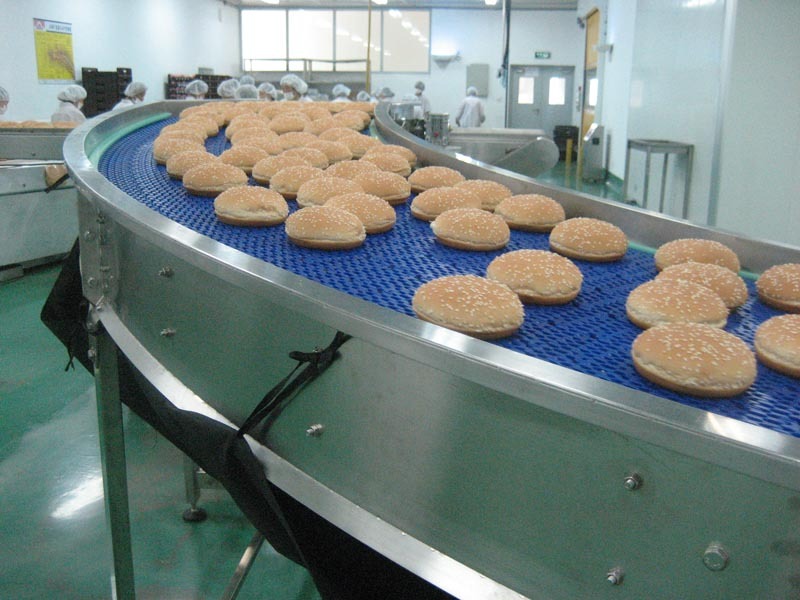
MatTop conveyor utilizes a continuous interlocking plastic or metal chain. The modular design allows it to navigate curves, inclines, and tight spirals while offering high durability and easy section-by-section cleaning or repair.
Case Conveyors
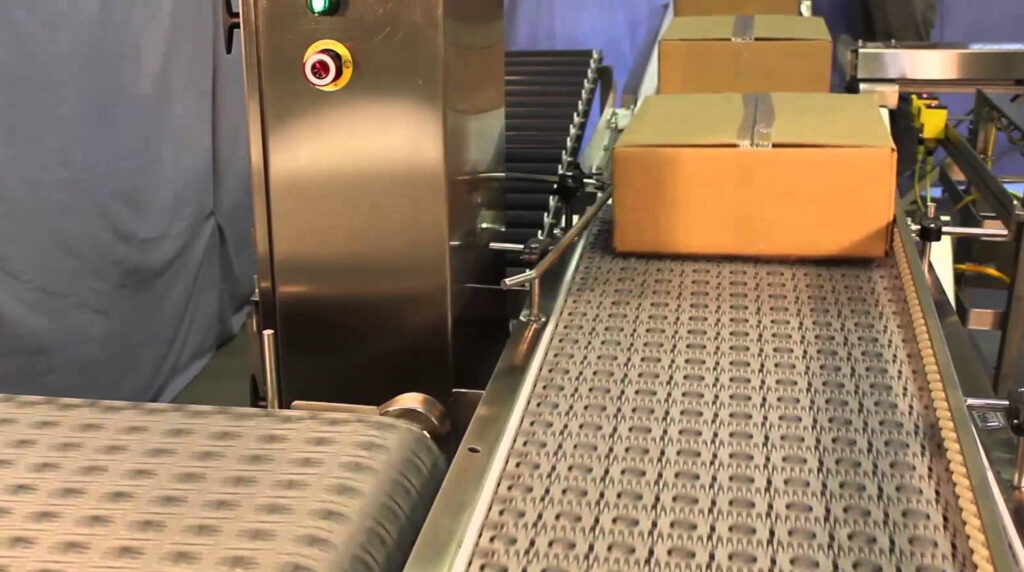
Case conveyors are automated systems designed to transport boxes, cartons, crates, and totes from one point to another in packaging and distribution facilities. They come in various configurations, including powered belt, gravity rollers, and spiral conveyors. Special equipment integrated to handle specific functions like taping, sealing, indexing, code reading, accumulation, diverting, or orientation change of the boxes/cases.
Stack Conveyors
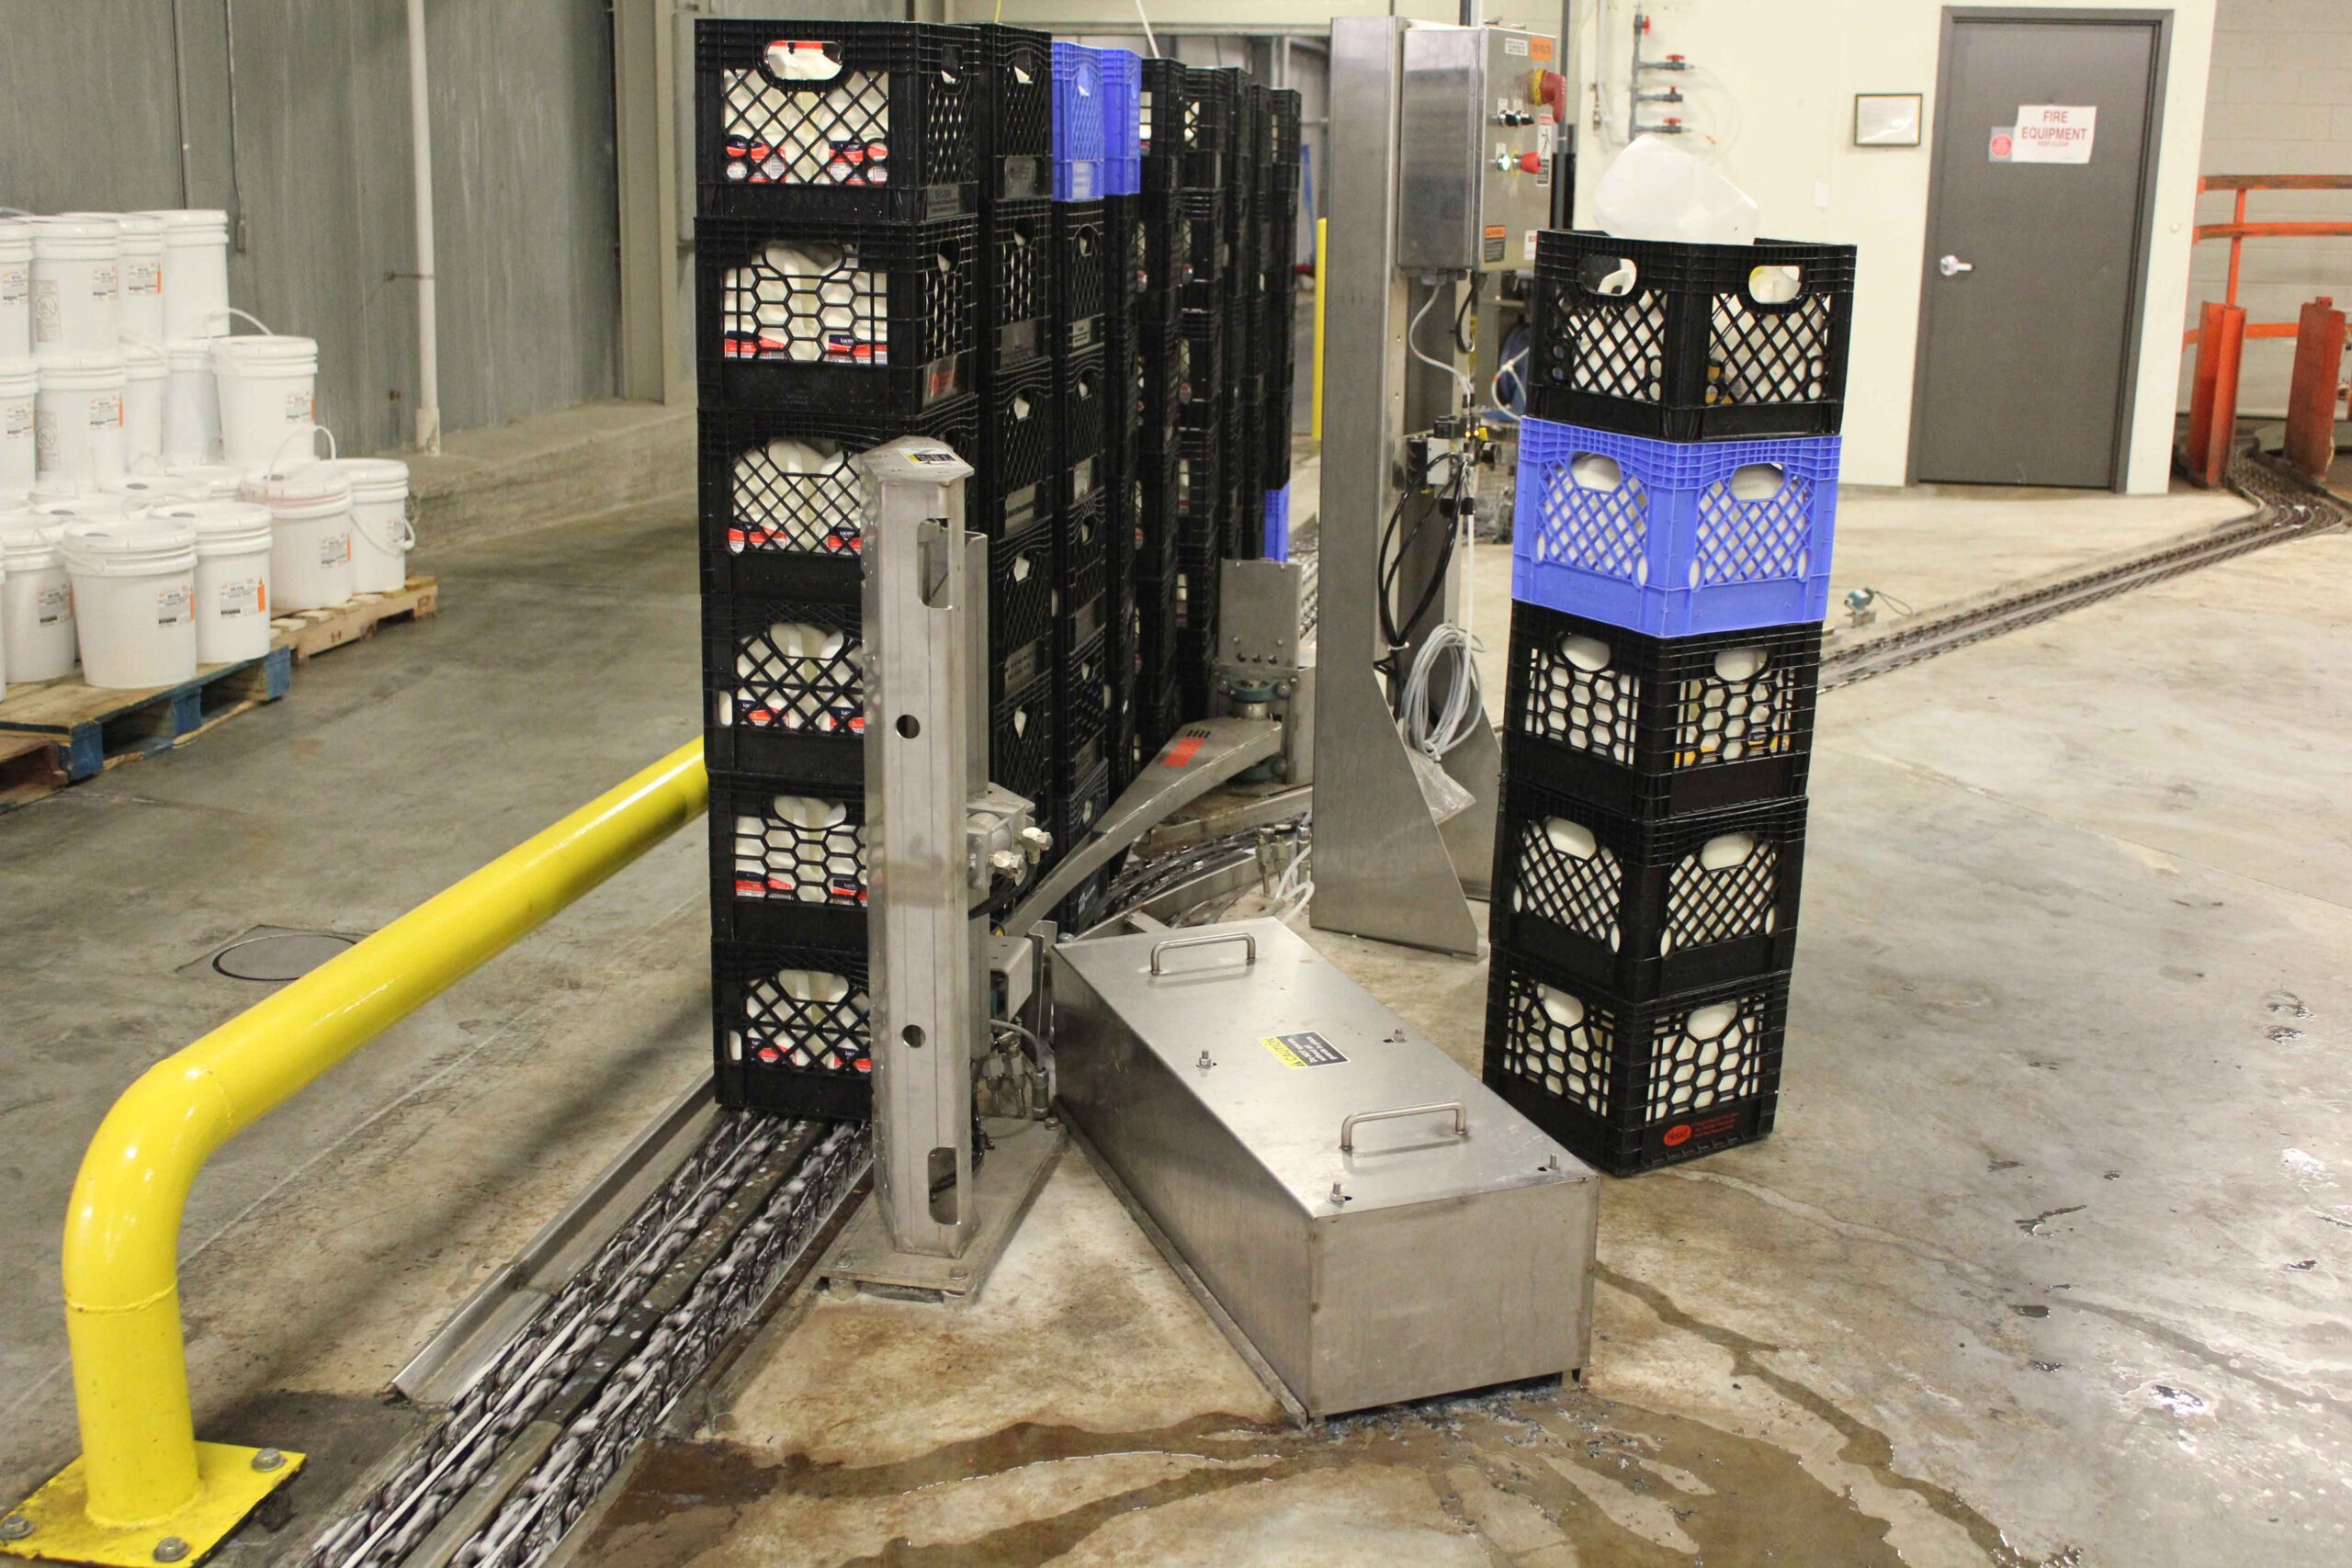
A milk crate stack conveyor is an industrial system that automates the handling, moving, and elevation of heavy plastic milk crate stacks. It keeps your dairy or beverage facility running smoothly, seamlessly transferring washed, empty, and filled cases between processing rooms, storage, and palletizing areas.
Incline/Decline Conveyors
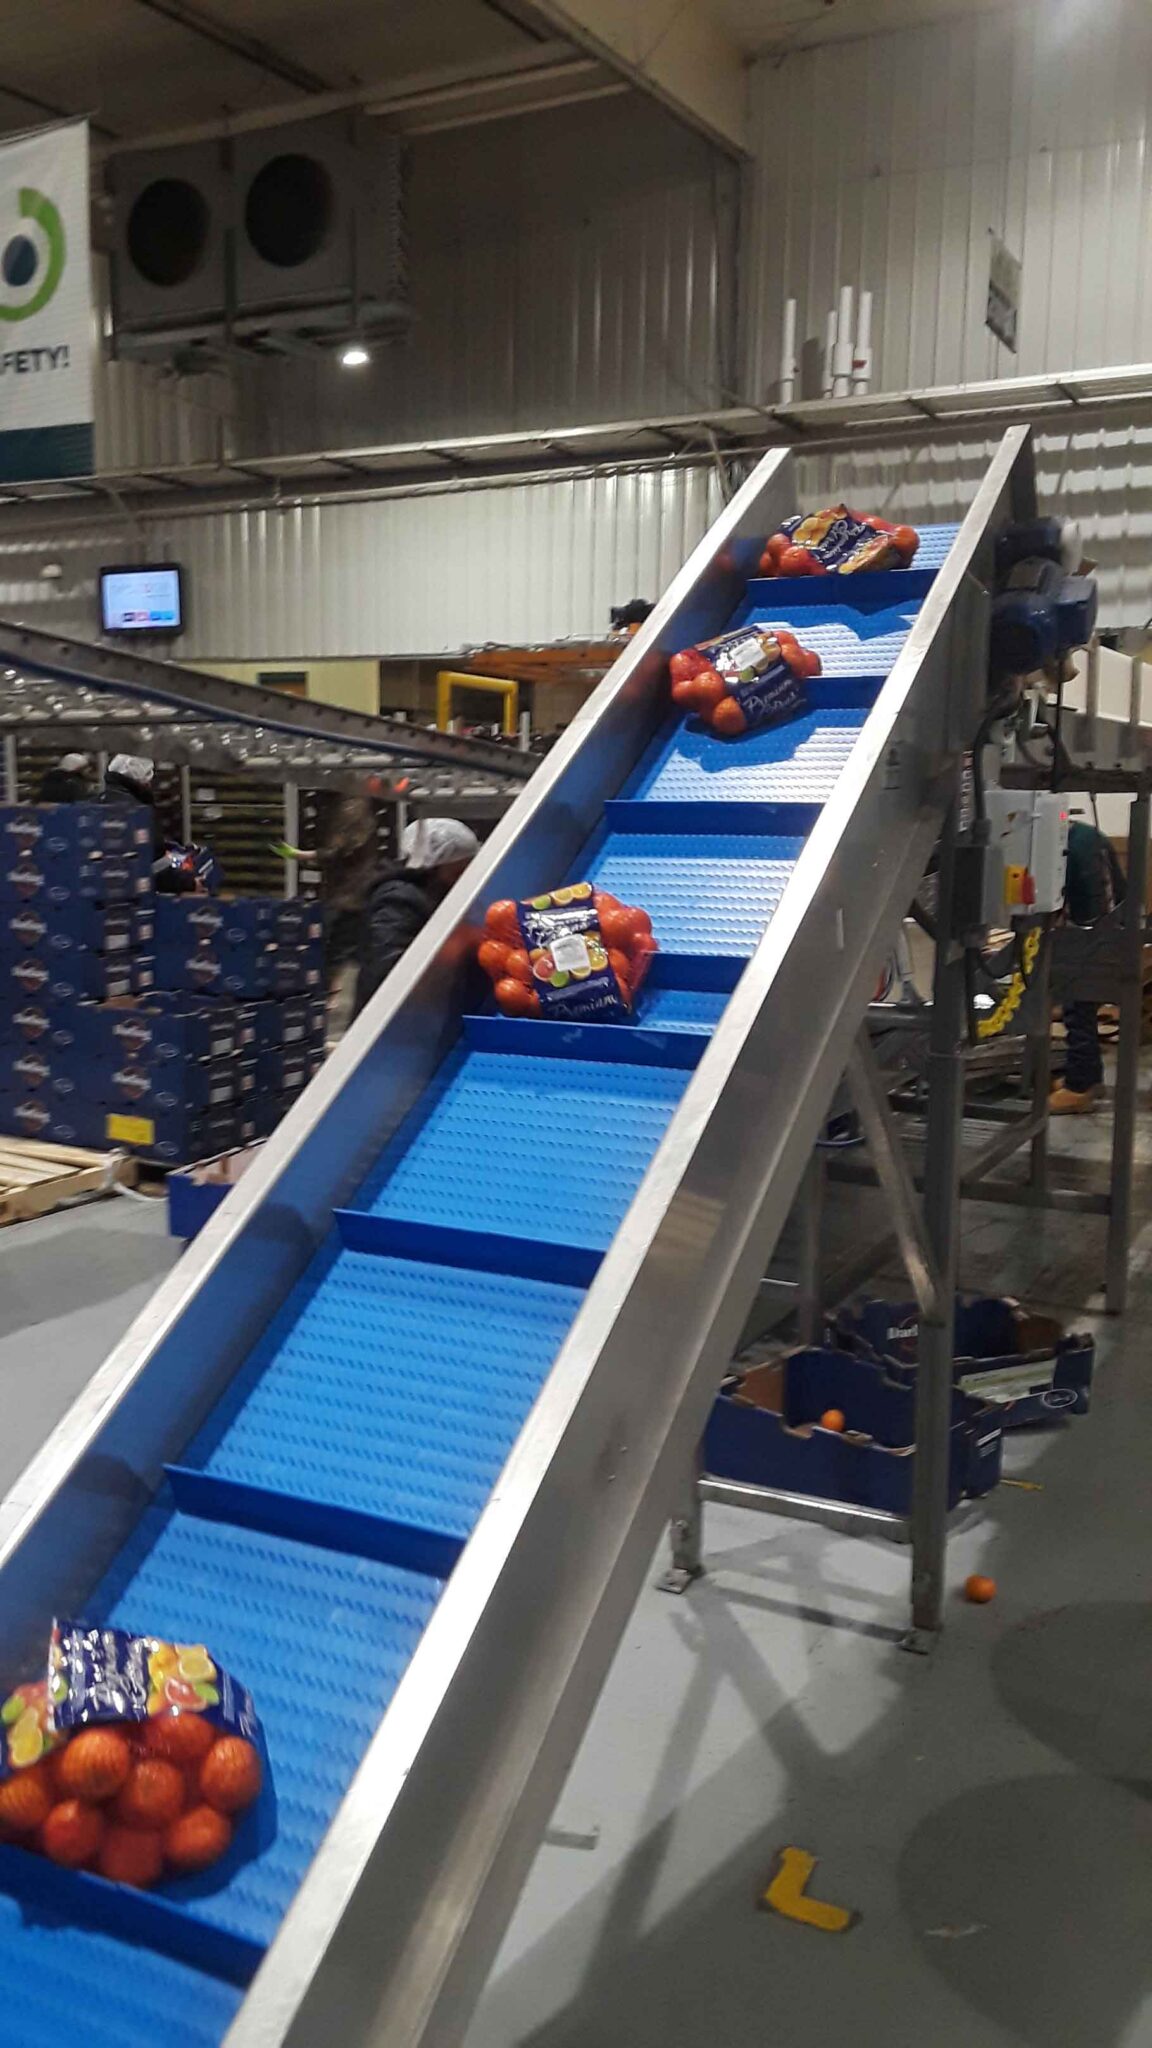
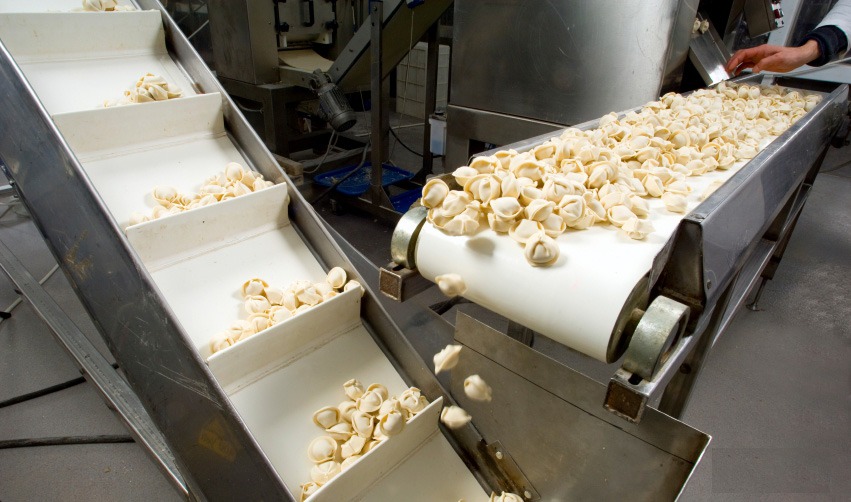
An incline/decline conveyor is a mechanical system designed to transport products or packages between different elevations. They are highly utilized in food and beverage processing and packaging to move goods between floor levels and elevated mezzanines, significantly saving space and reducing manual lifting.
Recycling Conveyors
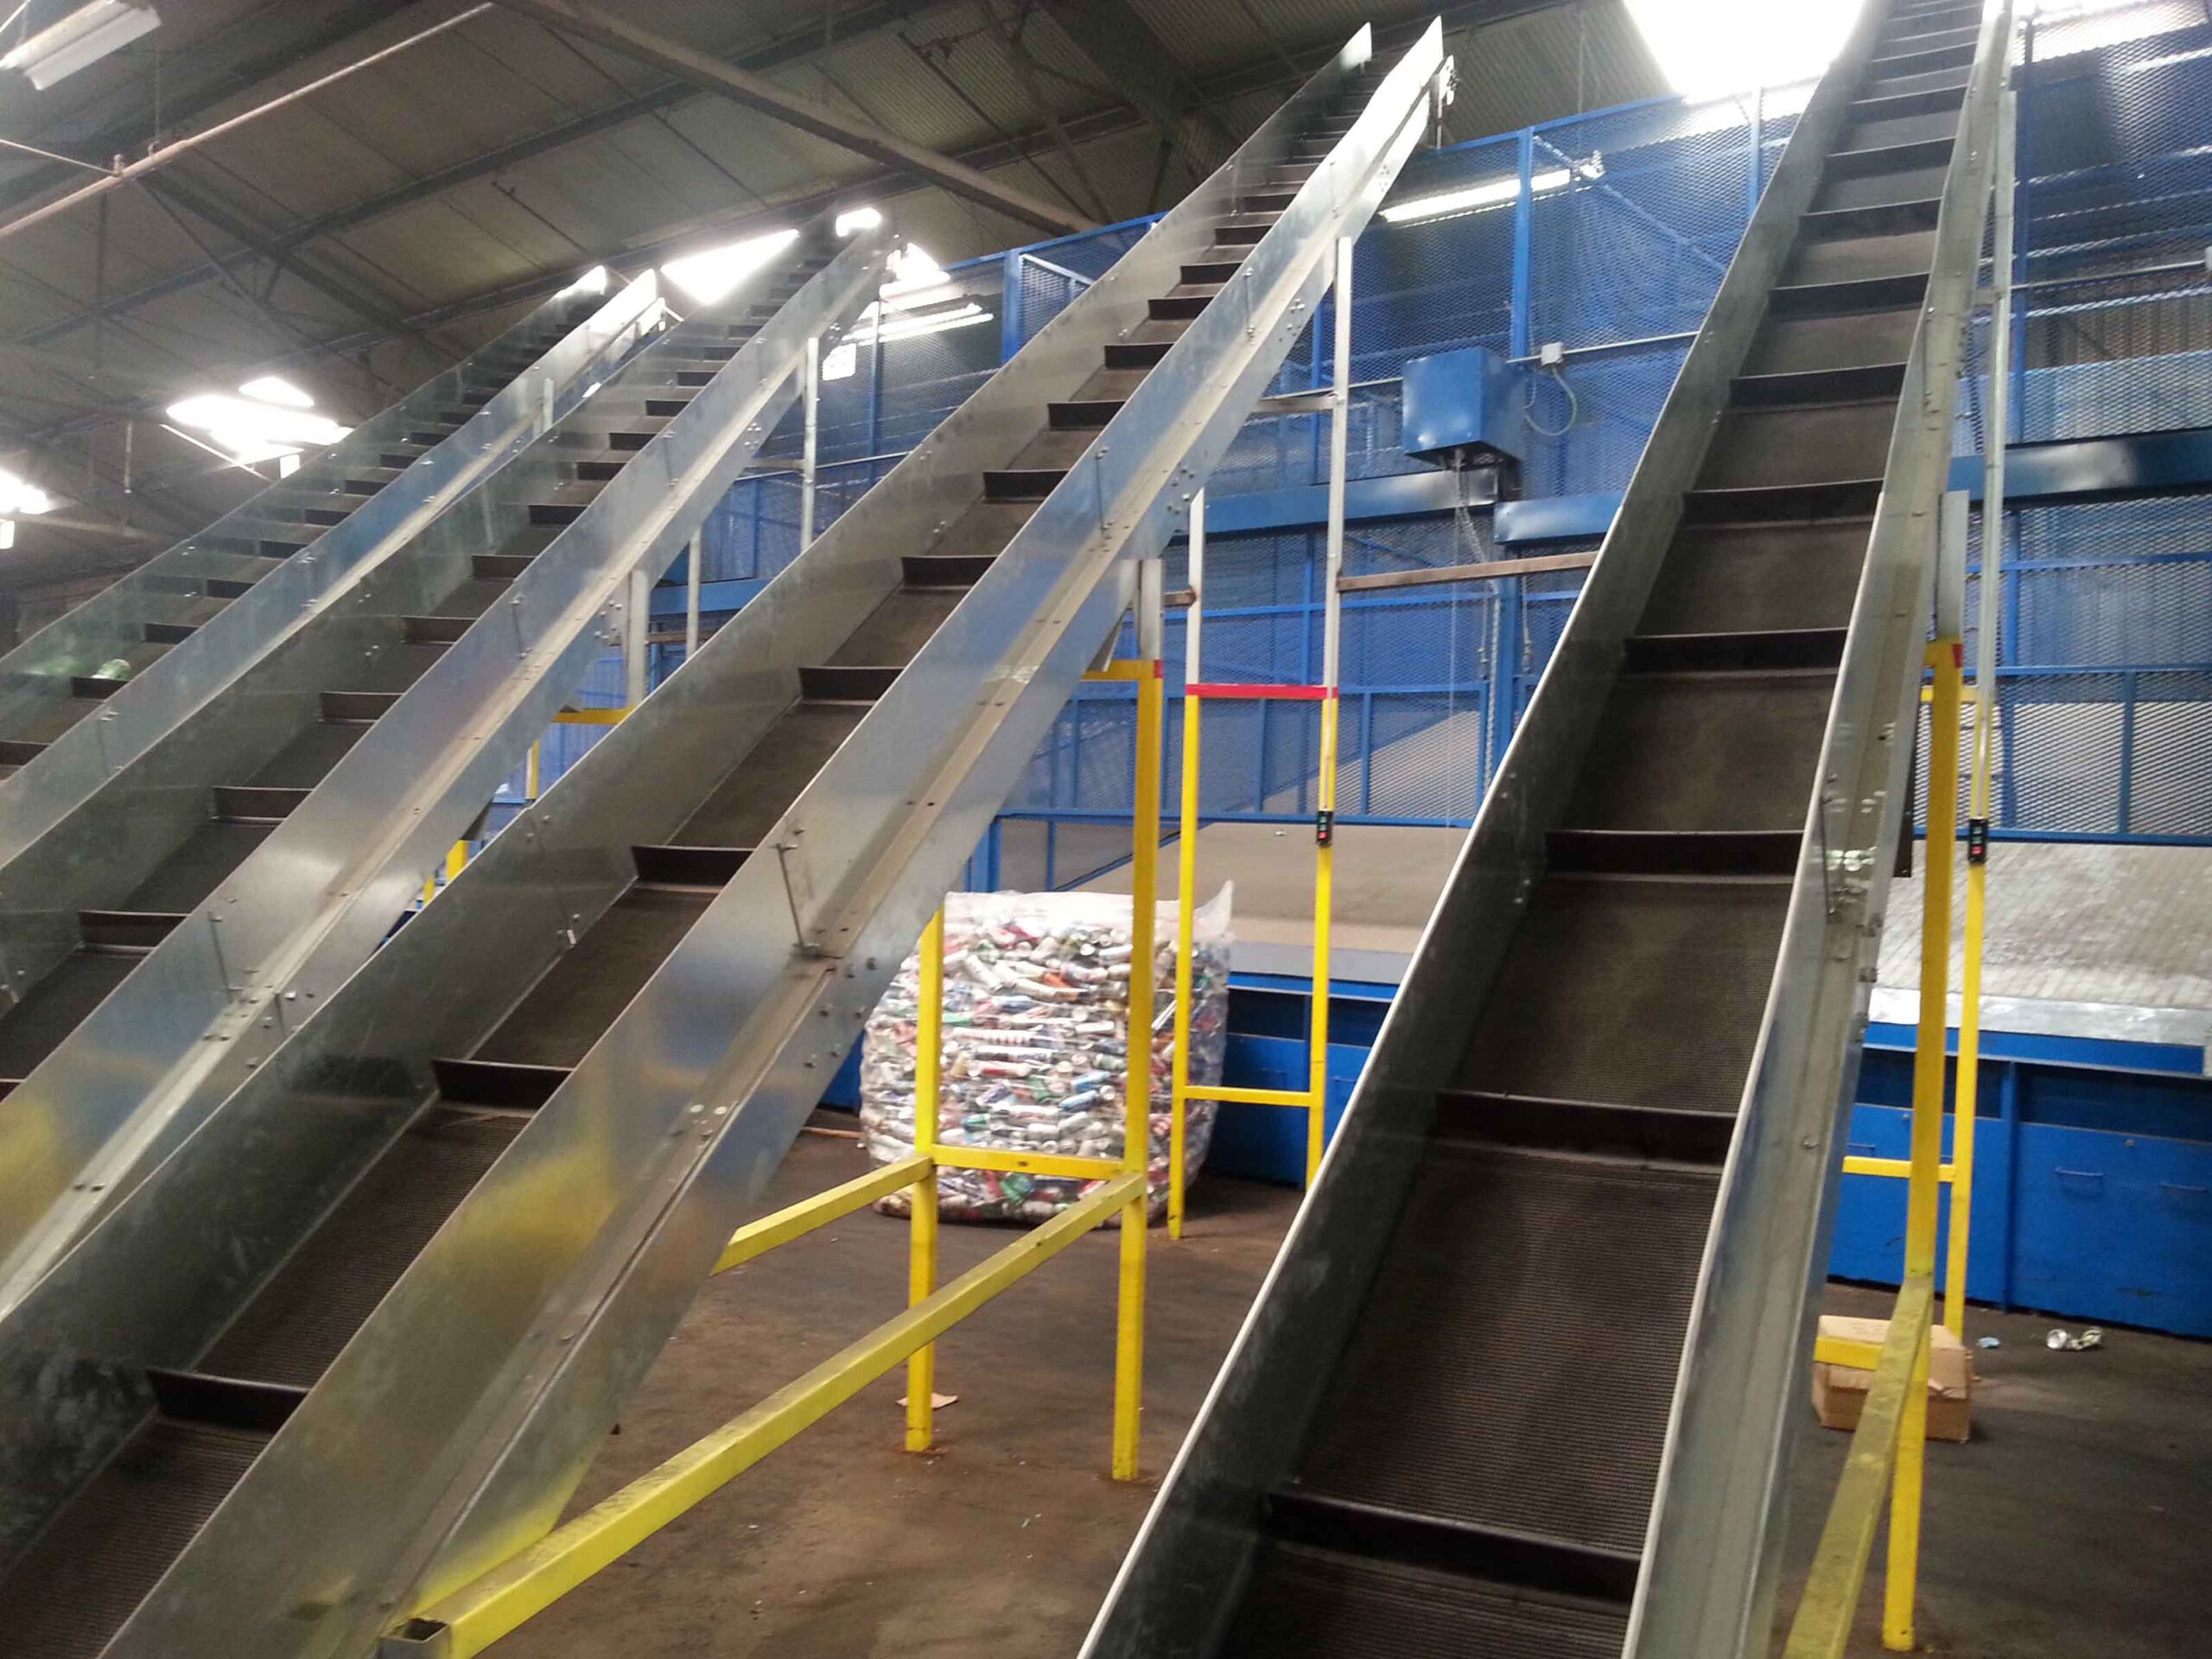
Recycling conveyors are automated systems designed to streamline waste sorting, shredding, and baling. They enhance safety and increase throughput by eliminating manual handling. Common configurations include inclined/slider-bed heavy-duty rubber belts for moving materials between levels, magnetic separator conveyors for pulling ferrous metals, and heavy-duty hinged steel belts for large scrap and mixed solid waste.
Wire Mesh Conveyors
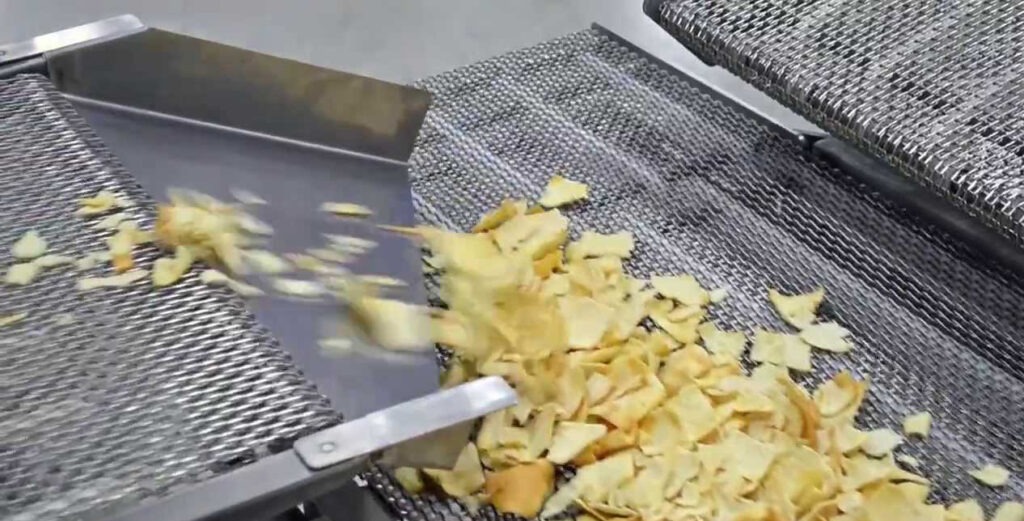
Wire mesh conveyors are heavy-duty industrial systems featuring interlinked metal wires, uniquely designed for extreme temperatures, washdowns, and processes requiring air circulation, forming an open, durable, and highly permeable surface. The open mesh provides ample open area, allowing items to heat, cool, dry, or drain easily while in transit.
Spiral Conveyors
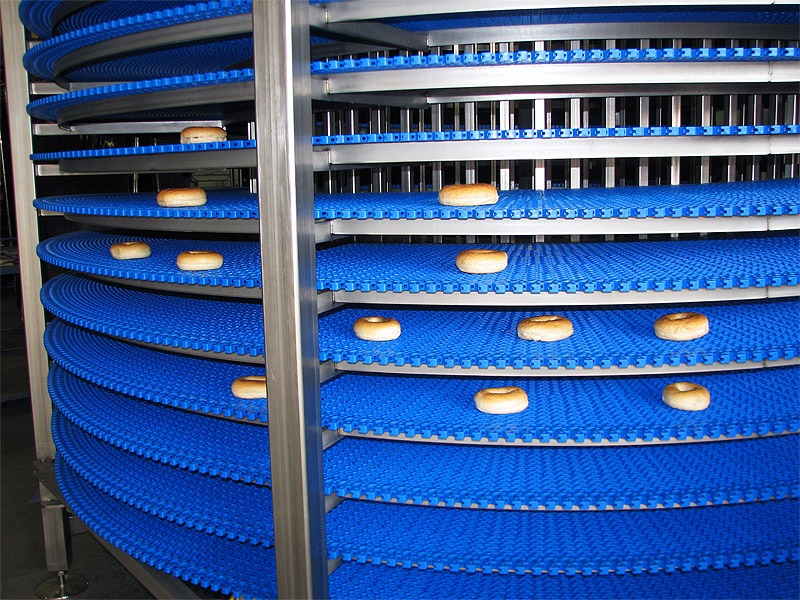
Spiral conveyors are vertical material handling systems that transport products continuously along a helical path around a central column. They save significant floor space compared to traditional incline belts and move items like cases, bottles, and totes between elevations seamlessly. Spirals at bakery plants are carrying hot bakery products for ambient cooling. Freezer spirals provide deep freezing of meat, pizza, ice cream and other products.
Endless Belt Conveyors
An endless conveyor belt is a closed-loop system manufactured or permanently vulcanized without mechanical fasteners, splices, or seams. This jointless design provides uniform tension and smooth operation, drastically reducing vibration, material snags, and wear on system components like pulleys. Endless belts are essential in applications that require high precision, sanitation, and uninterrupted movement.
Cable Conveyors
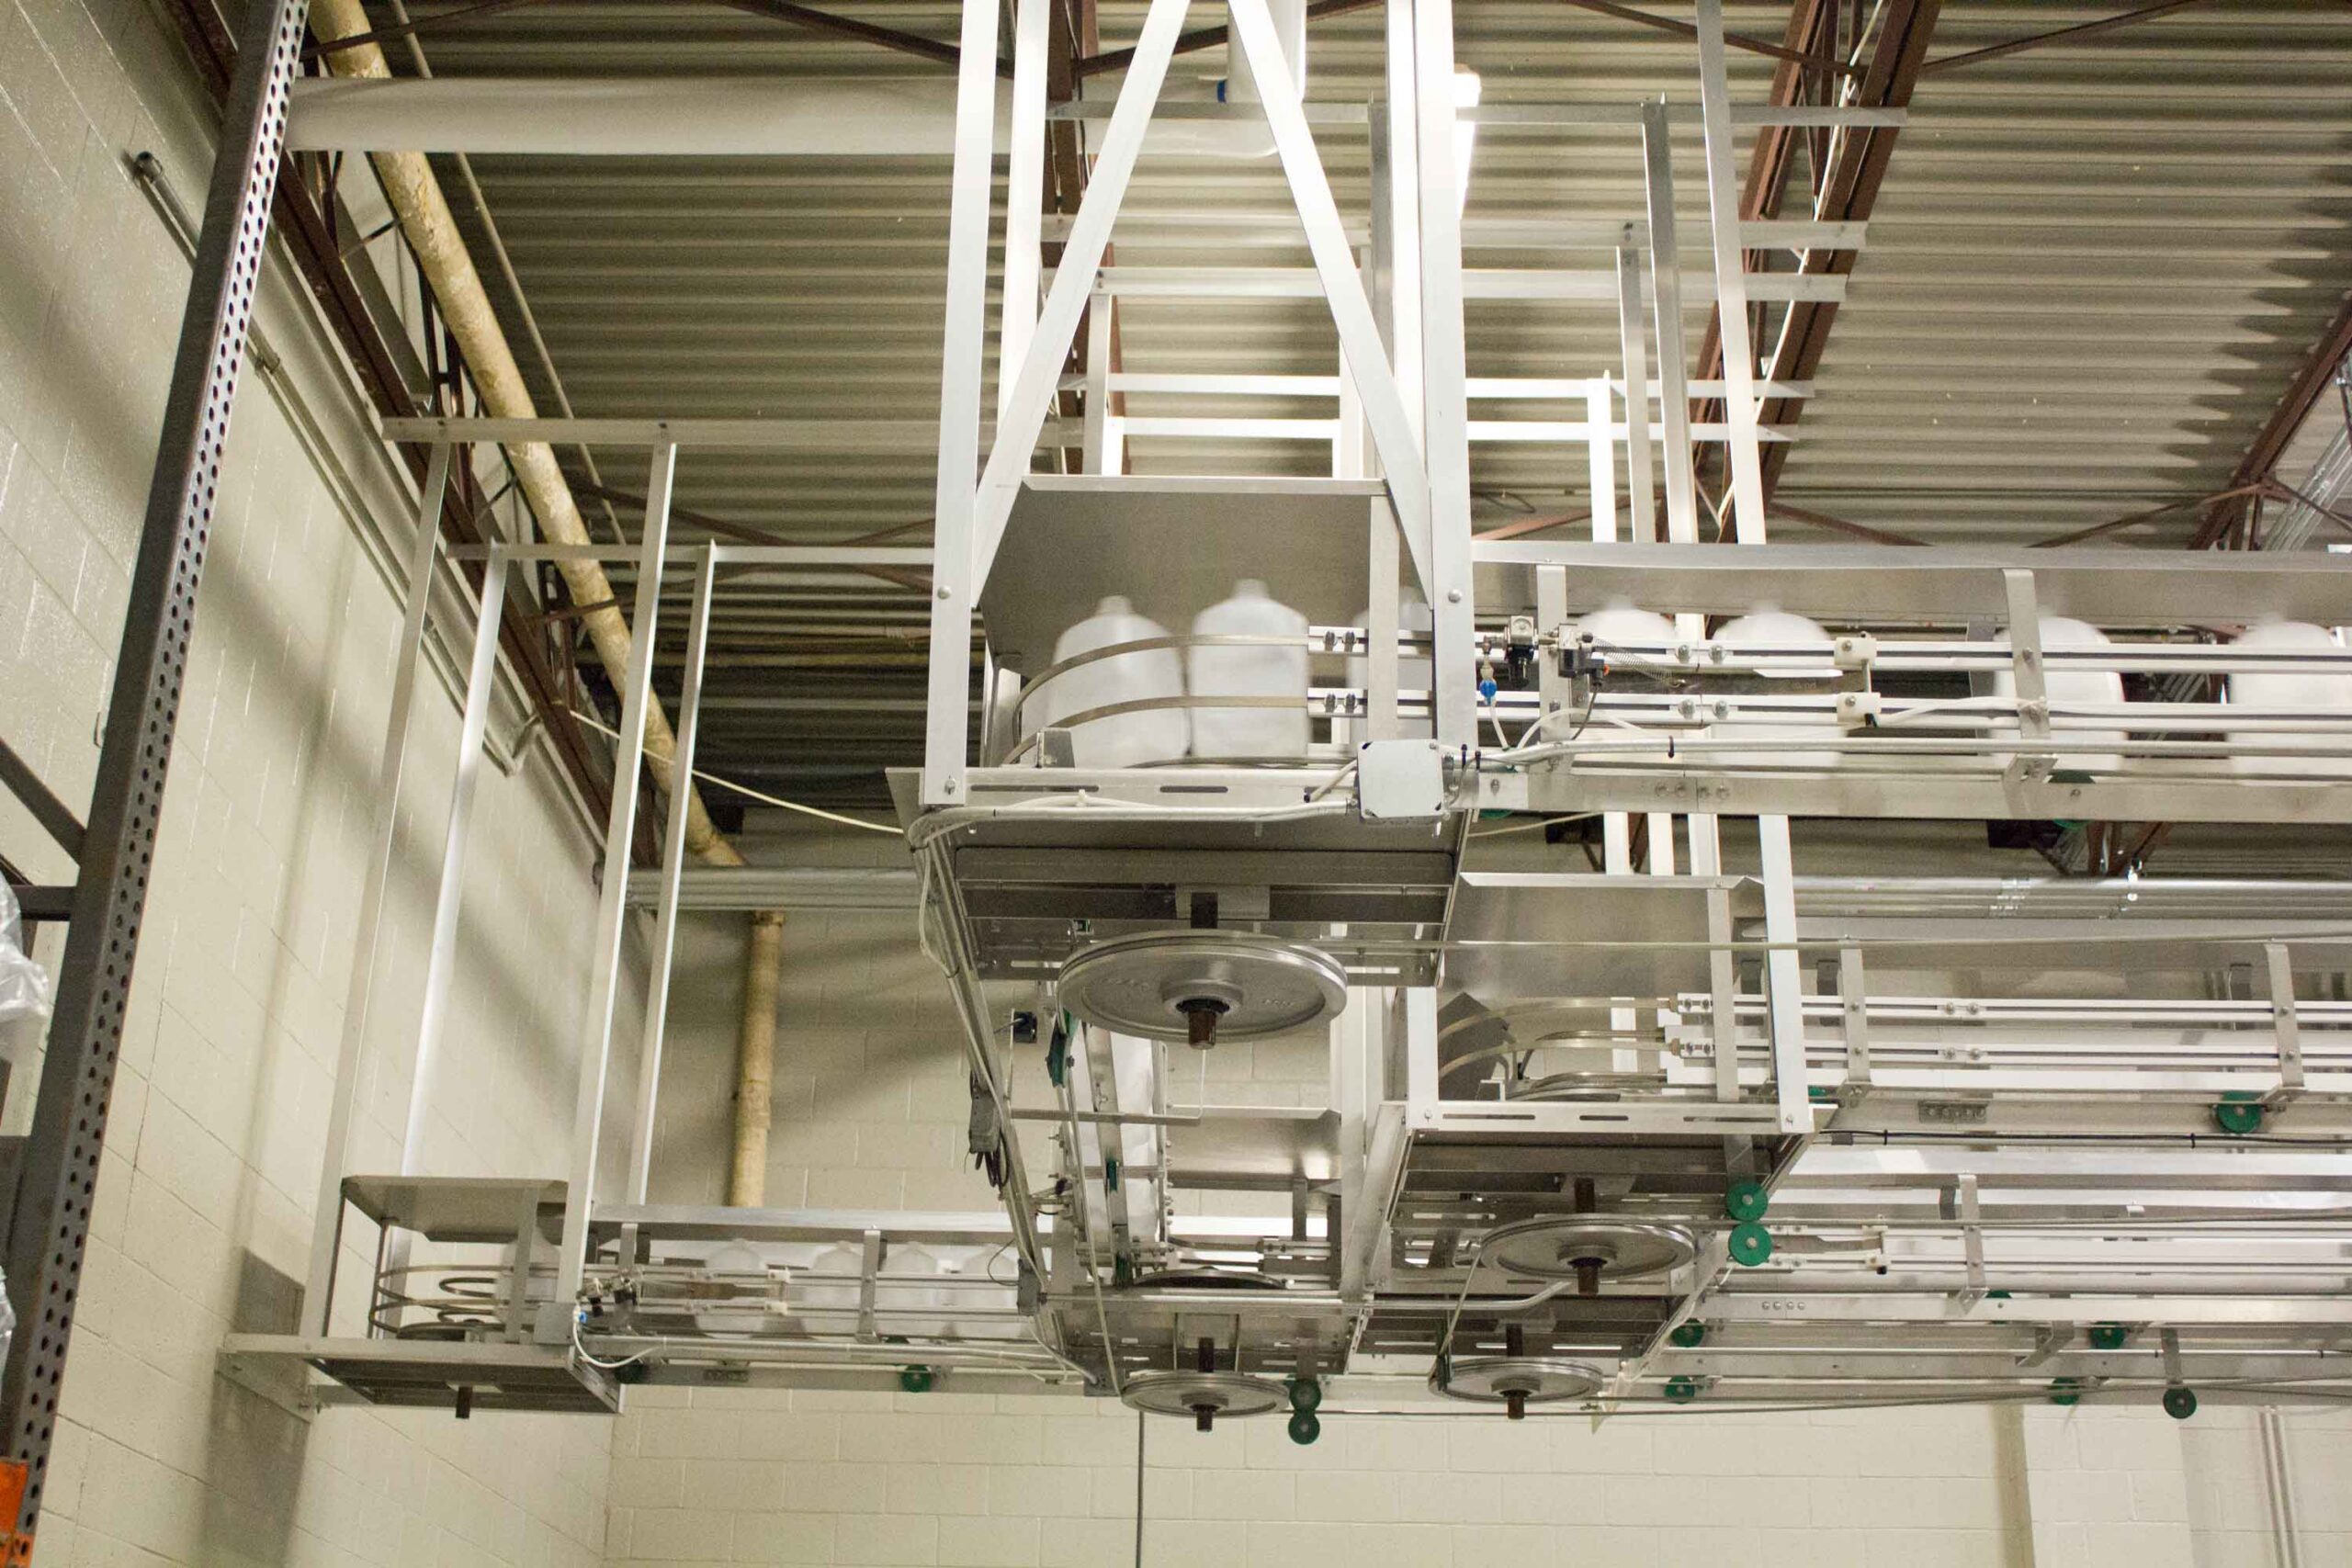
Specialized material handling system that uses a continuous loop of flexible cable with evenly spaced solid discs attached to it to move containers to the processing room. Mostly used for conveying empty bottles or jars from debagging to filling area. Cable conveyor is less costly alternative to mattop conveyor, running overhead without interfering with on-floor operations.